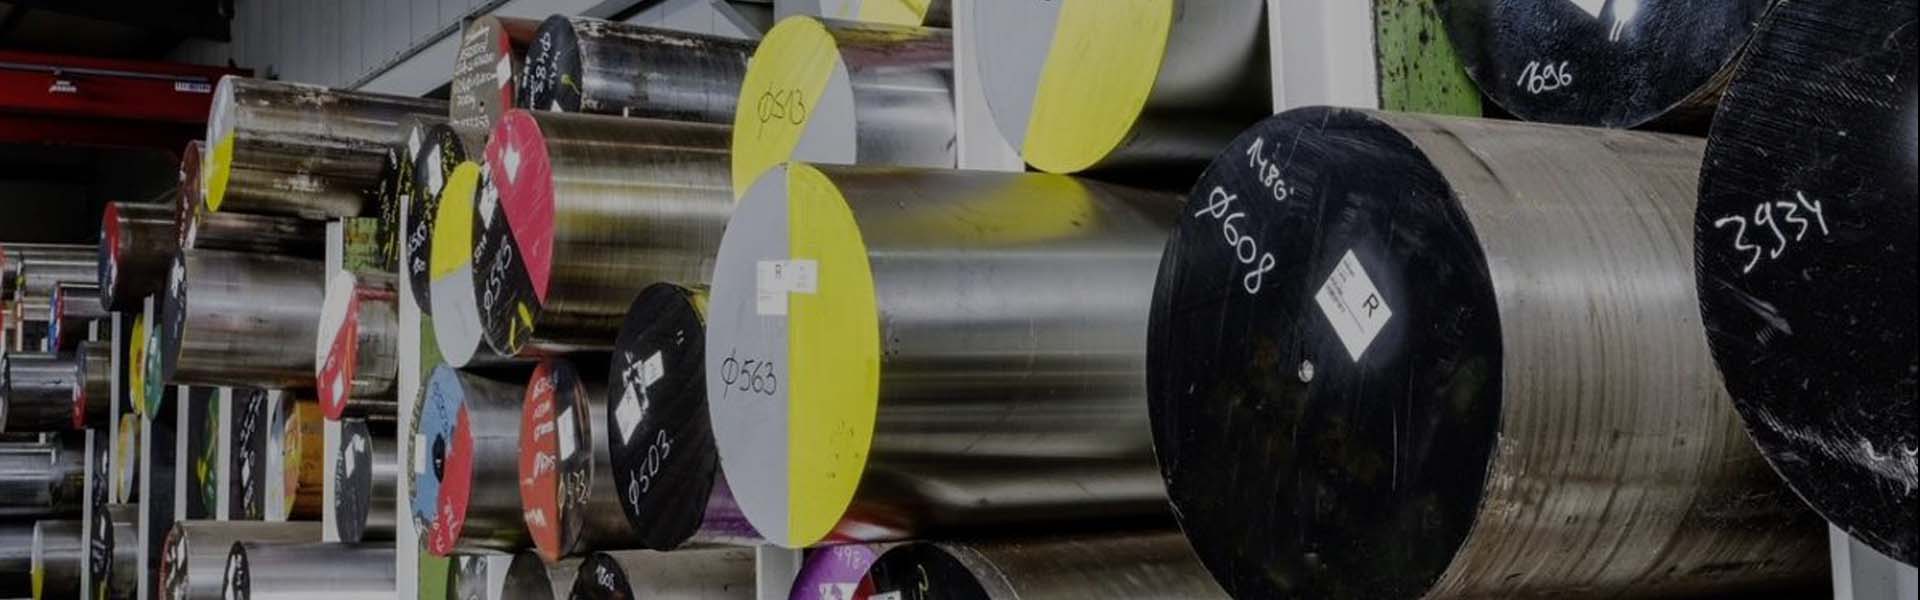
Toolman Special Steels is proud to produce and offer M2 (1.3343) - a medium alloy high speed steel with good machinability. The M2 alloy has somewhat better wear resistance than M1. In addition, it achieves a balance between toughness, wear resistance, and thermal hardness because of its alloy composition. It is widely used for cutting tools and other applications requiring high-performance materials. .
Steel Properties
-
Outstanding cutting hardness, wear resistance, and toughness at high temperatures
-
Special carbide precipitated during tempering at high temperatures and secondary hardening
-
Fine grain size
-
Uniform carbide
-
High toughness
-
Good toughness and cutting capability
-
Deep hardening response.
Chemical Composition
| Element | Value |
|---|---|
| C | 0.9 |
| Cr | 4.1 |
| Mo | 5.00 |
| W | 6.00 |
| Co | - |
| V | 1.8 |
Mechanical Properties
| Property | Value |
|---|---|
| Hardness (HBW) | 250 max (Annealed) |
| Quenching and Tempering Hardness (HRC) | 64 min |
Physical Properties
| Property | Value |
|---|---|
| Density (g/cm³) | 8.1 |
Modulus of Elasticity
| Temperature (°C) | kN/mm² |
|---|---|
| 20 | 225 |
Thermal Properties
| Temperature (℃) | Thermal Expansion Coefficient (10^-6/℃) |
|---|---|
| 400 | 12.1 |
| 600 | 12.6 |
Thermal Conductivity
| Temperature (℃) | Thermal Conductivity (W/m•K) |
|---|---|
| 20 | 24 |
| 400 | 28 |
| 600 | 27 |
HEAT TREATMENT AND PROCESSES
Heat treatment
| Heat Treatment Process | Temperature Range | Procedure | Purpose | Resulting Hardness (HRC) |
|---|---|---|---|---|
| Annealing | 850-880°C | Heat slowly to 850-880°C, hold until uniform, cool in the furnace to room temperature | To soften the steel and relieve internal stresses | - |
| Stress Relieving | 600-700°C | Heat to 600-700°C, hold until uniform, cool in still air | To remove machining stresses | - |
| Hardening | 1200-1250°C | Preheat to 450-500°C, then heat rapidly to 1200-1250°C, hold until uniform, quench in oil or air | To increase hardness and wear resistance | - |
| Tempering | 540-600°C | Heat to 540-600°C, hold for at least 2 hours, cool in still air | To balance hardness, strength, and toughness | 58-65 HRC |

Applications
-
Knives, thread cutting and twist drills
-
Broaching and milling tools, woodworking tools, cold working tools
-
Sendizimir rolls
-
Reamers circular saw segments
-
Cold forming like cold extrusion rams and dies
-
Plastic moulds with elevated wear resistance and screws
-
Mold applicaitons (screw mold, header punch, die)
Quality Assurance
Our M2 1.3343 steel undergoes rigorous testing and quality control to meet international standards, ensuring consistent performance and reliability. Certificates and test reports are available upon request. Feel free to reach out to us for more information on our M2 1.3343 steel products or to discuss your specific requirements. We're dedicated to providing top-quality steel solutions that meet your needs and exceed your expectations.
Manufacturing Range
| ROUNDS | SQUARES | ||
|---|---|---|---|
| SIZE (MM) | CONDITION | SIZE (MM) | CONDITION |
| 6.00 - 14.00 | CG | 7.2, 8.8, 10.5, 11 | HRA |
| 15.00 - 50.00 | HRAP | 13.5, 14, 17.5, 21 | HRA |
| 52.00 - 405.00 | FAT | 27, 32, 40 | HRA |
| 52.00 - 305.00 | FA |
Flats
| THICKNESS | WIDTH | CONDITION |
|---|---|---|
| 5.00 - 32.00 | 21.00 - 105.00 | HRA |
| 32.00 - 105.00 | 40.00 - 205.00 | FA |
Frequently Asked Questions
M2 / DIN 1.3343 / AISI M2 is a medium-alloy high speed steel with good machinability. Toolman describes M2 as offering a balance of toughness, wear resistance and thermal hardness, together with cutting capability and a deep-hardening response. These properties make it suitable for cutting tools and other high-performance tooling applications.
A maximum annealed hardness of 250 HBW for M2 and a minimum quenching-and-tempering hardness of 64 HRC under its mechanical properties. Its heat-treatment table separately lists a resulting hardness range of 58–65 HRC after tempering at 540–600°C.
We supply M2 for knives, thread-cutting and twist drills, broaching and milling tools, woodworking and cold-working tools, Sendzimir rolls, reamers, circular saw segments, cold-extrusion rams and dies, plastic moulds requiring elevated wear resistance, screws, header punches and dies.
Our published annealing range is at 850–880°C, stress relieving at 600–700°C, and hardening at 1200–1250°C after preheating to 450–500°C. Hardening is followed by oil or air quenching. Tempering is carried out at 540–600°C, with a hold of at least two hours followed by cooling in still air.
We offer M2 rounds from 6–14 mm, 15–50 mm and 52–405 mm, depending on the manufacturing condition. Squares include listed HRA sizes from 7.2–40 mm and forged-annealed squares from 52–305 mm. Flats range from 5–105 mm thickness and 21–205 mm width, depending on condition.
Chemical composition contains M2 with 0.9% carbon, 4.1% chromium, 5.00% molybdenum, 6.00% tungsten and 1.8% vanadium.
Yes. Our M2 / 1.3343 steel undergoes testing and quality control and that certificates and test reports are available on request. Manufacturers should communicate their grade, size, quantity and application requirements when making an enquiry.
